Let’s Start The Journey
What actually destroys synthetic lines the fastest? Abrasion ruins lines long before heavy tension does. Protecting that vital distance between core strength and surface wear matters most. Proper UHMWPE mooring rope construction resists harsh contact points. Discover optimal protective coatings and smart hardware maintenance strategies.
Quick Answer
Most synthetic mooring lines are not tension retired; they are abrasion retired. UHMWPE resists it by aligning molecular chains, having a slick surface, and through the application of coatings. Construction and hardware condition are as important as the fiber grade. Secure the points of contact and the core will outlive the vessel’s agenda.
- The abrasion resistance of coated HMPE is approximately 20% higher than when it is not coated.
- Specific gravity 0.97 means the line floats, avoiding seabed grit.
- Bend ratios of less than 15:1 D/d crush fibers and run up wear at the surface.
The Short Version
- The wet abrasion resistance remains excellent, with 0% loss of strength when HMPE is submerged.
- One 44mm HMPE line carries 133.6 metric tons MBL at low weight.
- When salt crystals sit in a dried braid, they behave like little blades.
- A sacrificial sleeve is much cheaper than replacing a 96mm hawser.
- If a line has had 10% diameter loss, or if there is fused glazed fiber, take it out and replace it.
Numbers Worth Remembering
- The elongation remains at 3-4%, so the shock transfers to hardware and not to fiber.
- The melting point is around 145°C, which is below the 260°C of polyester.
- Coated lines have survived 1,000 hours of ISO 4892-2 UV exposure.
- The weight advantage over steel wire runs about 85% lighter.
What Actually Wears a Mooring Line Down at the Chock?

Abrasion can be deadly on mooring lines long before tension is. Each tide cycle drags fiber across steel or concrete under partial load, and a line that is more or less never shock loaded will still have to be retired for surface damage. That rubbing removes material, creates heat, and opens the braid to grit.
On returned rope we continually observe the same three failure zones. The eye splice taper, the fairlead contact patch, and the initial one meter away from the winch drum. Everything else is generally new looking.
Here is the thing about friction. It does not have to be aggressive. A boat that travels 300mm on a swell, 6,000 times daily, will put a groove into a jacket more effectively than any storm can. The real enemy is that slow grind, and that is why the UHMWPE properties get referenced in terms of how they behave on the surface, not just in tensile numbers.
⚠ Warning: If a rope tests bad visually at the splice taper, it most likely is bad along the whole working section. Never re-splice and redeploy.
Before reading on, pose yourself these two questions. Honestly speaking, how rough are your chocks these days? And when was the last time anyone ran a hand along the full length of your primary lines?
Fibre Anatomy: What Sits Inside the Braid
The simple UHMWPE rope meaning is that which is directly derived from the chemistry. To make polyethylene behave less like plastic and more like structural fiber, the chains have to be long enough, and that is ultra-high-molecular-weight polyethylene. Most maritime documentation refers to the material as high modulus polyethylene, and it is indeed the same material.
- Chain Alignment: Gel-spinning aligns the polymer chains almost parallel, and that is where the strength comes from.
- Fiber Density: The finished UHMWPE fiber rope has a specific gravity of 0.97, which signifies that it floats in seawater.
- Surface Character: A drawn filament that is smooth and waxy, giving the naturally low UHMWPE friction coefficient.
- Moisture Behavior: Wet UHMWPE rope strength is essentially equal to dry, with water absorption being very low.
That is how UHMWPE applications have come about across the same basic fiber, from ship mooring to deep-sea aquaculture, heavy lifting to off-road recovery. The same molecule, jacketed in a variety of ways.
There is one disinterested thing to be said first. The fiber melts around 145°C and polyester takes 260°C. That difference is not academic at a winch drum generating friction heat during a long payout, and we will return to this point.
UHMWPE Mooring Rope’s Abrasion Resistance Explained!

This is the part to mark. Nine mechanisms working in parallel, each performing part of the task, each having a different failure mode when it is outright ignored.
1. Molecular Chain Alignment Lets the Surface Shear Rather Than Snag
In parallel chains, the abrading edge slides across the plane of the filament rather than catching a raised loop and tearing it out. That one piece of structure distinguishes high performance ropes from commodity synthetics, and it is why a thinner HMPE line will sometimes last longer than a thicker polyester line on the same chock.
- Shear Over Snag: Along aligned filaments, the rough edge does not hook and break the filaments.
- Fewer Loose Ends: With tight molecular packing, there is virtually no fiber to grab onto with the hardware.
- Even Load Sharing: Aligned chains share load, so no single filament is subjected to a spike.
- Predictable Fuzzing: Surface damage is observed as uniform fuzz, and that is much easier to inspect than random cuts.
2. A Low Friction Coefficient Keeps Heat Out of the Core
Elevation of temperature from friction will occur at much lower temperatures than the melting temperature of polyethylene, and frictional heat is an inducement to melting.
Less rubbing ends up as less thermal energy, and because the fiber surface is slick, glazed areas on a well-specified line are usually a sign of hardware issues rather than fiber issues. We do not consider glazing to be a fault.
- Cooler Contact Patches: Smaller friction means a smaller temperature increase in a smaller area over a longer winch payout.
- Reduced Internal Rub: The smooth internal filaments, which are in contact with one another in the braid, do not fuse to one another.
- Easier Hardware Passage: The line renders through low drag fairleads with less manpower.
- Early Warning Signal: A hard, shiny glazing typically indicates that the roller is seizing, and not that the rope has deteriorated.
3. Coating Chemistry Does Work the Bare Fiber Cannot
Bare HMPE is slick but not armored. The interstitial areas are filled with a coating based on polyurethane, which obstructs the penetration of salt and increases the hardness of the surface. Our DMX coating provides about a 20% increase in abrasion resistance, plus a proven longer life, which on a 96mm hawser results in substantial savings per berth cycle.
- Salt Barrier: The coating ensures that abrasive crystals never make it to the load-bearing core of the braid.
- Surface Hardening: On the first run, a cured polymer layer takes the concrete and rusted steel instead of the fiber.
- Internal Lubrication: Strand-on-strand friction during dynamic cycling is decreased by coating between the strands.
- UV Shielding: Treated lines have maintained structure after 1,000 hours of continuous ISO 4892-2 exposure.
4. Braid Geometry Decides Where the Wear Actually Lands
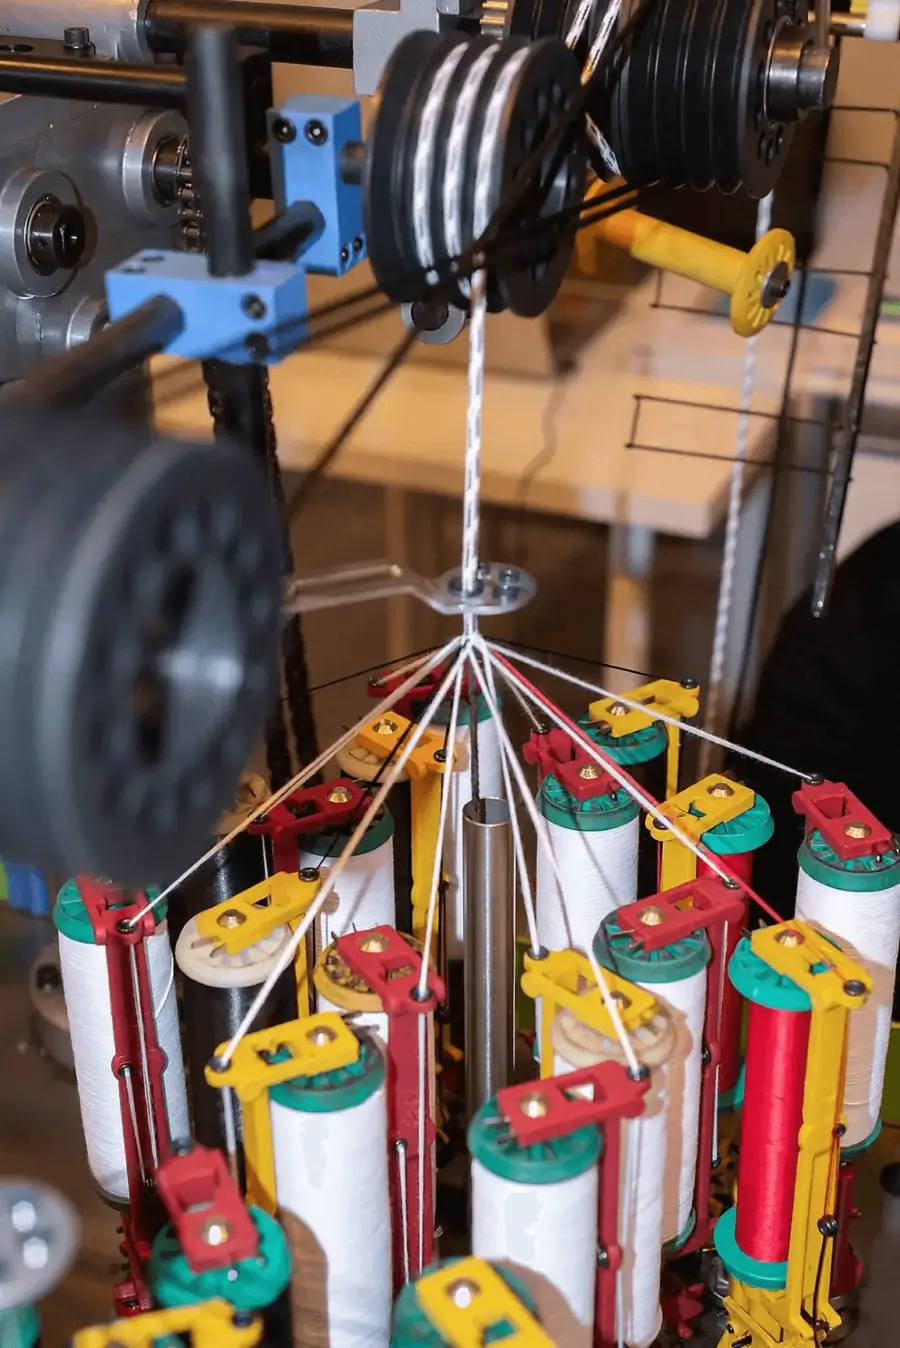
Most buyers do not realize just how much the contact geometry is changed by construction. The 12-strand single braid will flatten out under tension and spread a load over a wider footprint. Double braid retains its round shape and focuses tension on a smaller surface area. They both fail, there is no right or wrong, they are simply different.
- Flattening Behavior: Compared to a round profile, 12-strand spreads contact pressure over more surface area under working load.
- Jacket Sacrifice: Double braid always loses the cover first without altering the core.
- Torque Neutrality: Balanced plaited constructions defy rotation and stop the twist that opens braids to grit.
- Splice Geometry: A tapering approach helps prevent the combined stress peak from abrasion and fatigue.
⚠ Pro Tip: Match construction to hardware, not price. To lose the whole point of the jacket, simply run a double braided UHMWPE rope on a smooth split drum.
5. Wet Abrasion Behaves Nothing Like Dry Abrasion
When saturated, the softening and weakening of polyamide by about 10-15% also reduces its abrasion resistance. HMPE stays dry and absorbs virtually nothing. Practically speaking, that translates to a line performing on a rain-soaked deck at 0300 exactly as it performed on a dry bench, and after all, that is the real world.
- Zero Absorption: There is no moisture uptake into the fiber, so mechanical properties remain unchanged while it is submerged.
- Consistent Weight: Wet mooring rope weight does not climb, and handling effort stays predictable for crew.
- No Softening: The filament surface remains hard and resistant, not soft, when wet.
- Freeze Resistance: Dry fiber does not aggravate the ice-loading of saturated ropes in winter ports.
6. Bend Ratio at the Fairlead Creates Hidden Internal Damage
There is a very good reason why OCIMF MEG4 prescribes a minimum D/d ratio of 15:1. Tighten the rope and the outer strands stretch out while the inner strands contract, squashing fibers against each other. What you do not notice until the line parts is the wear inside, and that makes it the most dangerous wear mode on any deck.
- Fifteen To One: To prevent crushing, a bend’s diameter should be at least 15 times the diameter of the rope.
- Compression Damage: A tight small radius crushes inner filaments where no visual inspection will ever see them.
- Roller Condition: Rolling contact is immediately transformed into pure sliding abrasion by seized fairlead rollers.
- Cumulative Effect: Fatigue occurs in the bend gradually over thousands of tides until it bursts.
7. Salt Crystallization Is the Abrasive Nobody Budgets For
Water evaporates from the lines and leaves the seawater behind as crystals of sodium chloride inside the braid. Those crystals lie between strands with edges that can cut individual filaments during the next dynamic stretch. Freshwater flushing is low cost and remains the greatest return on investment maintenance practice we recommend to fleet operators.
- Crystal Formation: As water from seawater dries, crusty corners of salt are left inside the braid structure.
- Internal Cutting: Crystals cut the filaments when they are stretched from end to end, which cannot be seen from outside the jacket.
- Monthly Flushing: Deposits are dissolved with a freshwater rinse before they build up in damaging quantities.
- Coating Defense: Crystals will not enter properly treated marine lines because of sealed surfaces.
8. Sacrificial Protection Beats Sacrificing the Rope
We do not want to sell you a new hawser, we would love to sell you a sleeve. Tubular nylon guards, hook-and-loop wear protection, and chock sleeves absorb friction at known wear points and are replaced in minutes. Our nylon guards are able to perform to 250°C, well in excess of what the underlying fiber could handle.
- Removable Guards: Velcro closure sleeves move along the line with the movement of the contact points as tides rise and fall.
- Chock Protection: HD polyester sleeves protect the rope as it goes through metal fairleads.
- Heat Headroom: Nylon protection withstands 250°C, long before the fiber would soften.
- Cost Ratio: The cost of replacing a sleeve is a small percentage of taking a larger diameter mooring line out of service.
9. Retirement Thresholds Turn Judgement Into Procedure
Fuzz is normal. Fuzz is even protective, as raised surface fiber cushions the core below. Measurable diameter loss is the main cause of retirement, along with cut strands that take out more than a quarter of the cross-section, hard glazed sections, and chemical discoloration. The written thresholds take the argument off the deck.
- Ten Percent Rule: If the diameter loss is more than 10%, the line is withdrawn from service immediately.
- Strand Count: Cut strands greater than one quarter of the cross-section mean retirement, not repair.
- Glaze Detection: The hard, fused areas show heat damage that is not discernible from outside.
- Logged Hours: Recorded deployment hours turn subjective inspection into an auditable retirement decision.
Construction Types and How Each One Wears

Various types of braids break in different areas. This is not the marketing wear profile; it is the wear profile that we actually see on product returned to us.
| Construction | Contact Behavior | Primary Wear Zone | Splice Difficulty | Best Fit |
| 12-Strand Single Braid | Flattens under load, wide footprint | Uniform surface fuzz | Low, hollow core accepts bury | Split-drum winches, main mooring |
| Double Braid | Holds round profile | Outer jacket sacrificed first | High, twin-path bury | Rough concrete bollards, high chafe |
| 8-Strand Plaited | Torque neutral, lays flat | Strand crowns | Moderate | Warping heads and capstans |
| Parallel Core | Zero constructional stretch | Jacket only | Specialist | Static terminal securement |
| Coated 12-Strand | Sealed surface, low ingress | Coating layer first | Low | High-salinity working berths |
We have always recommended a working mooring using a 12 strand UHMWPE rope, and the flattening action actually works. It is more contact surface, so less pressure per square millimeter, and less pressure means slower wear. If there is rusted steel or unfinished concrete, we use a jacketed build and pay up the higher UHMWPE rope price to cover our bases.
⚠ Pro Tip: Any UHMWPE braided rope laid over a wire-grooved drum will wear out in a few weeks. Before it goes on line, fit smooth sleeves.
Materials Weighed Against the Alternatives

Knowledge of the various types of mooring ropes provides a means to avoid over-specifying one type and under-specifying another. Nylon has great shock absorption, and when wet it does not abrade well.
Polyester comes up trumps for UV and friction resistance, but it is heavier and has a lower ratio of strength to weight. Steel wire is difficult to cut, and it kinks and recoils with lethal force.
| Material | Specific Gravity | Elongation | Wet Strength Loss | Abrasion Resistance | Melting Point |
| UHMWPE (HMPE) | 0.97 (floats) | 3-4% | 0% | Excellent | 145°C |
| Nylon (Polyamide) | 1.14 (sinks) | 20-30% | 10-15% | Good, poorer wet | 215°C |
| Polyester | 1.38 (sinks) | 12-18% | 0% | Very good | 260°C |
| Polypropylene | 0.91 (floats) | 15-25% | 0% | Fair | 165°C |
| Steel Wire | 7.85 (sinks) | Under 1% | Corrodes | Good, kink-prone | Not applicable |
Does Buoyancy Change How a Line Wears?
Yes, and more than it gets credit for. The often-asked question about does Dyneema float follows directly from that 0.97 figure, and the answer is that HMPE floats, which means it avoids contact with seabed sand, shell fragments, and hardware dropped from the boats. A sinking line drags across whatever the harbor bottom is made of, and harbor bottoms are like sandpaper.
During tug work, floating also eliminates the possibility of propeller entanglement, a fact that is of great importance long before the point where wear rates come into it.
On the UHMWPE vs Dyneema Question
Customers enquire about UHMWPE vs Dyneema every week. Dyneema is not a separate material, it is a brand of HMPE fiber. A quality Dyneema mooring rope and a quality unbranded HMPE line share the same polymer chemistry, and the differences that matter are fiber grade, coating, braiding tension, and whether the manufacturer break tests batches. Our tip is to request the test certificate rather than the name of the brand.
Sizing Guide: Diameters, Weights and Breaking Loads

Under-sizing is dangerous and over-sizing is a waste of drum capacity. These are working figures from our range of HMPE rope, useful for anyone who wishes to specify a marine mooring rope against vessel displacement.
| Diameter (mm) | Circumference (inch) | Weight per 100m (kg) | Breaking Strength (ton) | Breaking Strength (kN) |
| 24 | 1 | 37 | 38 | 371 |
| 32 | 1-5/16 | 62.5 | 68.5 | 671 |
| 40 | 1-5/8 | 87 | 98.2 | 964 |
| 44 | 1-3/4 | 96 | 118 | 1158 |
| 48 | 2 | 114 | 139 | 1364 |
| 64 | 2-5/8 | 209 | 222 | 2178 |
| 80 | 3-1/4 | 328 | 333 | 3266 |
| 96 | 3-5/9 | 509 | 455 | 4463 |
Note the weight column. At 44mm you are carrying 96kg per 100 meters, whilst the same in steel would weigh many times more for comparable strength. That is where the 85% figure comes from, and that is why UHMWPE synthetic rope replaced wire on most decks during the past 10 years.
It is not as though color was only about beauty either. A black UHMWPE rope blends in with the grease and grime that get onto the working deck, and a blue UHMWPE rope provides a good contrast with white fiberglass and grey steel for night time work. We provide both, as well as red, green, grey and white.
How Long Does a UHMWPE Line Last Before Retirement?
With proper specification, coating and protection, the working service life of an HMPE mooring line is typically five years. In high-salinity ports, uncoated lines run closer to two. The environment and the hardware condition are so overwhelming that the difference is that wide, and it is not the fiber grade doing it.
| Condition Observed | Severity | Action | Typical Cause |
| Light uniform fuzz | Normal | Continue service | Routine surface contact |
| Diameter loss under 5% | Monitor | Log and reinspect monthly | Progressive fairlead wear |
| Diameter loss over 10% | Critical | Retire immediately | Sustained abrasion, poor hardware |
| Hard glazed patches | Critical | Retire section or line | Friction heat, seized rollers |
| Cut strands over 25% | Critical | Retire immediately | Sharp edge contact |
| Discoloration, stiffness | Investigate | Sample test | Chemical or UV exposure |
Documentation requirements for mooring rope regulations under OCIMF MEG4 and SOLAS inspection procedures call for documented line management, not memorized management. The breaking loads stated on the certificate are based on the physical test methods specified in ISO 2307. Three standards, one practical outcome: keep records or lose out in a port audit.
⚠ Warning: A line that passed 12 months ago is worth nothing today. Retirement decisions are based on deployment hours, not on calendar age.
Inspection and Handling Tips That Buy Extra Seasons

Real gains are achieved through unglamorous habits. The recurring preventable damage that our service team sees on returned product year after year traces back to four or five things being left out.
- Freshwater Flushing: Flush lines every month to dissolve salt crystals before these can slice into the fiber.
- End-For-End Rotation: Rotate lines each year, allowing wear to spread rather than concentrate.
- Hardware Polishing: Sand fairleads to 400 grit and file every burr you find.
- Dry Ventilated Storage: Store coils out of direct sunlight in an airy deck locker.
- Sleeve Repositioning: Shift chafe guards in conjunction with the movement of the contact point through tidal fluctuation.
On splicing, crews frequently ask about how to splice UHMWPE rope in the field. A hollow 12-strand accepts a standard bury splice with an aluminum fid, and the bury length must reach 21 fids to avoid slip under load. A proper eye splice holds about 90% of the listed strength. A knot will hold about half. Avoid tying knots in lines that are being used to moor.
For what it is worth, my old bosun swore by the daily runs we would make along the first 10 meters with our bare hands. He caught more internal damage that way than anyone ever caught with a checklist.
What We’d Put on Your Bollards?
Where Generic Lines Fall Short
- Uncoated Import Stock: Fiber with no polyurethane treatment absorbs salt within the few weeks following delivery, and it is generally used up on a high-salinity berth in less than two years.
- Bargain Jacketed Builds: Loose cover-to-core bonding allows jackets to bunch during payout and concentrate the friction in one place, destroying the line at that point.
- Wire Replacements Sized by Habit: When replacing steel with synthetic, the same diameter is generally too much for the drum’s capacity, and it simply dismisses the different bend radius requirements altogether.
- Unbranded Fiber Without Batch Data: If there is no break-test certificate attached to your individual spool, then the printed MBL is not a measurement, it is a claim.
What We Recommend Instead
- Coated Mainline for Working Berths: marine mooring rope in coated 12-strand construction handles daily tidal cycling, floats readily away from seabed grit, and carries the DMX treatment for that 20% abrasion gain.
- Crew Protection on Manned Decks: anti-snap mooring rope builds an energy-absorbing core within the line, so a parting under load drops to the deck instead of recoiling back through the snapback zone.
- High-Cycle Buoy and Pendant Work: HMPE Mooring Pendant comes from 12mm to 44mm with breaking strengths ranging from 121kN to 1158kN, spliced to 6, 8, 10 or 15 feet to order.
- Surge-Exposed Ports Needing Stretch: Mooring Tail Rope in nylon or polyester-polypropylene blend provides added elasticity in front of the rigid mainline and safeguards the deck hardware from shock, in accordance with OCIMF MEG4.
- Offshore Terminal Loading: single point mooring hawser is manufactured in sizes from 80mm to 256mm with grommet MBL reaching 2411 tons, built for tanker transfer where nothing else is close.
Inside Duracordix: Capability Beyond the Coil
We are not a rope supplier. We are a synthetic rope solution provider, and that is reflected in what we do before the order is placed rather than after.
Engineering and Testing Depth
- In-House Break Testing: Each lot is subjected to destructive tensile testing on our own equipment, and the data ships with the lot rather than waiting on request.
- Certification Coverage: ABS, DNV, BV, CCS, ClassNK, LR and RINA approvals are held, with OCIMF MEG4 alignment across the mooring range.
- Coating Development: The DMX formulation was developed from our own testing on salt ingress and surface hardness, tested to ISO 4892-2 for 1,000 hours of UV exposure.
- Six-Stage Production Control: Fiber selection, twisting, braiding, coating, heat treatment and testing are all done in-house, so quality control happens at every process and not at the final inspection stage.
Solution Support, Not Just Supply
- Specification Consulting: Provide the working conditions and we suggest material, construction, diameter, MBL, eye splice design, protective sleeving, packaging and delivery arrangement as one package.
- Custom Build Capability: Working our own lines as a UHMWPE rope manufacturer, we are able to produce non-standard diameters, lengths, colors and splice configurations without treating them as an exception.
- Sample Evaluation: 7 to 14 days for sample assessment prior to commitment, because no one should purchase a mooring system from a data sheet alone.
- Delivery and After-Sales Coordination: Bulk production runs 30-45 days, urgent stock ships in 5-10, and the technical team stays available after delivery rather than disappearing once the invoice is sent.
Applications include marine mooring, offshore operations, towing, lifting, fishing and aquaculture, 4×4 recovery, industrial safety and construction. The same field of engineering, but varying working conditions.
Companion Gear Worth Specifying Alongside
Ordered as a system, these items can reduce replacement frequency significantly more than a fiber upgrade will.
Deck-Side Protection
- Wear Sleeving: Chafe Protection is available as tubular sleeves, hook-and-loop Dura Guard, PR wear protection and HD polyester chock guards, in sizes 6mm to 110mm.
Lifeboat Safety
- Fall Prevention Device: Fall Prevention Device combines 24mm HMPE braid with 6.5T shackles at 30T breaking strength, and meets IMO MSC.1/Circ.1327 and SOLAS standards.
Towing Duty
- UHMWPE Towing Rope: UHMWPE Towing Rope sits alongside on the mooring fiber platform, with diameters from 12mm to 96mm and breaking strengths ranging from 121kN up to 4463kN.
Reach Extension
- Reach Extension: A UHMWPE winch rope extension adds working length before purchasing a longer primary line, available in 1/4″, 3/8″ and 1/2″ at 50 feet.
Beyond the Mooring Deck
- Fishing and Aquaculture: Trawl Warps and HMPE Fish Cage netting use the same fiber chemistry against constant abrasive drag.
- Lifting Operations: Crane Rope and UHMWPE-D Round Sling provide a strength-to-weight ratio eight times that of steel, with a 5:1 or 7:1 safety factor.
- Vehicle Recovery: Soft Shackle and UHMWPE tow rope sizes run from 5mm at 8,200lbs up to 18mm at 95,000lbs.
- Forestry Transport: Synthetic Log Wrapper in 3/8″ will accommodate 18,500lbs at approximately one-third of the weight of steel wrappers.
People Also Ask
What Is HMPE Rope?
High modulus polyethylene is the same material that is used for UHMWPE. Both describe gel-spun polyethylene fiber made of aligned molecular chains, which provides steel-equivalent strength at roughly one-seventh the weight.
What Are The 6 Types Of Mooring Ropes?
Six are common: UHMWPE, nylon, polyester, polypropylene, polyethylene and steel wire. Each differs in buoyancy, stretch and abrasion resistance, so the choice depends on berth conditions and not on habit.
What Is The Best Rope For Mooring Lines?
UHMWPE suits high-tension commercial berthing. Nylon suits surge-exposed ports needing shock absorption. Long-term tropical berthing is achieved through polyester. No one fiber is a clear winner in all applications.
Does UHMWPE Rope Really Float?
Yes. Specific gravity of 0.97 is less than seawater, which causes the line to float. That prevents seabed abrasion and eliminates the possibility of propeller entanglement during tug operations.
How Much Abrasion Resistance Does Coating Add?
Around 20%. DMX coating fills interstitial spaces, blocks salt penetration and hardens the surface, extending service life measurably on high-salinity working berths.
Does UHMWPE Lose Strength When Wet?
No. Water absorption is negligible, making the wet strength equal to the dry strength. By comparison, nylon will lose 10-15% of tensile capacity when it is completely saturated.
What Bend Ratio Should I Maintain?
Minimum 15:1 D/d under OCIMF MEG4. The bend diameter must reach 15 times the rope diameter, otherwise inner filaments crush without any external indication.
When Should I Retire A Mooring Line?
Retire at 10% diameter loss, cut strands exceeding 25% of the cross-section, hard glazing, or chemical discoloration. Logged deployment hours guide the decision alongside visual inspection.
How Long Does UHMWPE Mooring Rope Last?
Five years typically for coated, protected lines. Uncoated lines in aggressive ports run closer to two. Hardware condition and maintenance dominate the outcome.
Can I Splice UHMWPE Myself?
Yes, on 12-strand hollow braid. Use an aluminum fid and bury 21 fid lengths minimum. A properly made eye splice holds about 90% of the rated strength.
Why Does My Rope Have Glazed Patches?
Friction heat. The fiber softens near 145°C, and seized fairlead rollers or fast payout under load generate enough heat to fuse surface filaments together.
Do Salt Crystals Really Damage Rope?
Yes. Evaporating seawater leaves angular crystals inside the braid that cut filaments during dynamic stretch. Monthly freshwater flushing prevents accumulation entirely.
Is Dyneema Different From UHMWPE?
No. Dyneema is one brand of UHMWPE fiber. The chemistry is identical, so compare fiber grade, coating quality, braiding tension and batch test data instead of brand names.
What Diameter Do I Need?
Measure by vessel displacement and windage, not by habit. A 44mm HMPE line carries 133.6 metric tons MBL and weighs 96kg per 100 meters.
Can UHMWPE Replace Steel Wire Directly?
Typically, yes, at a reduced diameter. Install smooth drum sleeves first, since wire-grooved drums shred synthetic fiber within weeks of installation.
Conclusion
Even premium synthetic lines eventually wear out. Proper sizing, protective sleeves, and strict inspection routines buy valuable operational time. Understand that every UHMWPE mooring rope relies on smooth chocks and clean fairleads to survive harsh coastal environments. Visit Duracordix online to explore expert solutions, review our marine product range, and secure safe vessel operations today.
About The Author

Moses Xu
VP & Technical Marketing Director
With over 10 years of hands-on experience in high-performance synthetic fiber technology, I help global clients—from professional racing teams to maritime engineering companies—to create unique and special fiber solutions by using high-performance UHMWPE, Kevlar, Nylon fiber, etc. Let’s help you for the next project and solve all your pain points together
 English
 Español
 Deutsch
 Français
 العربية
 한국어
 Русский
 Ελληνικά
 Italiano
 Português
 日本語
 Türkçe
 Tiếng Việt
 简体中文
 Suomi
 Svenska